ASFROM Gantry Cutting Machine FAQ
ASFROM Gantry Cutting Machine FAQ
Gantry Cutting Machine Base Q&A
I. Grundlegende Produktinformationen
Q1: What is SY‑830B Automatic Gantry Cutting Machine?
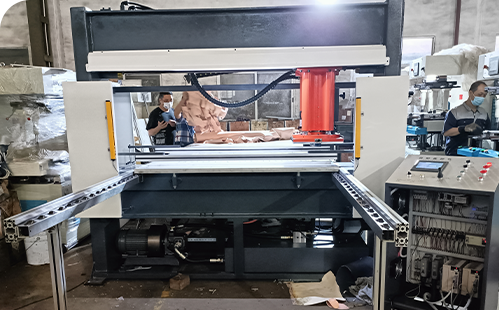
A1: SY‑830B Automatic Gantry Cutting Machine is a 30‑ton CNC servo‑driven gantry‑type automatic cutting machine. It adopts steel‑welded gantry frame, PLC‑servo control system. The cutting head moves horizontally by servo motor, feeding platform moves forward‑backward automatically with positioning accuracy up to 0.1 mm. It supports multi‑die layout in one setup, three cutting‑arrangement modes, touch‑screen parameter setting and recipe save / recall. Equipped with safety light‑curtain protection. External 0.6 MPa compressed air is required for material‑clamping mechanism. Target for mass‑production with low die‑change frequency. Up‑stream connects laminator, fabric‑inspection & rewinder. Cut parts go to inspection and sewing processes. Extension: Full‑series cutting‑machine comparison
‑ AFC‑622:22 T swing‑arm type, manual swing‑arm for small‑part sampling & small‑batch.
‑ AFC‑525 / 525A:25 T flat‑bed, manual die‑placement for medium‑small batch.
‑ AFC‑740:40 T four‑column;
AFC‑780:80 T four‑column. Four‑column models have no servo traveling head and require manual die‑change.
‑ SY‑830B:30 T automatic gantry, servo traveling head for auto die‑arrangement; for mass‑production with infrequent die‑change; large footprint and requires compressed‑air supply.
Q2: What are the core technical parameters of SY‑830B Automatic Gantry Cutting Machine?
A2:
1.Model No.: SY‑830B
2.Max cutting force: 30 T
3.Stroke: 5‑150 mm
4.Effective cutting area:1700×1600 mm
5.Moving‑head size:350×350 mm
6.Servo‑motor power:3 kW
7.Oil‑pump motor:5HP / 3.75 kW
8.Total power:7 kW
9.Power supply:3‑phase 220V /50 Hz
10.Hydraulic‑oil filling:80 kg
11.Machine dimension:5000×2500×2350 mm
12.Machine weight:3200‑3400 kg
13.Working air pressure:0.6 MPa
Extension: Avoid continuous full‑30‑ton operation which accelerates cylinder‑seal aging. Single die outer dimension shall not exceed moving‑head dimension 350×350 mm.
Q3: What are the main features of SY‑830B Automatic Gantry Cutting Machine?
A3:
1.PLC‑servo CNC system with servo cross‑travel head and auto‑feeding platform; positioning accuracy 0.1 mm. Support multi‑die layout and automatic die‑arrangement punching.
2.Touch‑screen HMI for setting ram angle, position, cutting speed, cutting depth and lifting height. Support recipe save & one‑click recall for different products.
3.Steel‑gantry frame with high rigidity & anti‑deformation. Fully‑automatic workflow: feeding‑cutting‑discharging.
4.Safety light‑curtain protection: machine stops immediately when human body intrudes working zone for operator safety.
5.Multi‑operation‑modes: inching, manual, semi‑auto, auto. Operator only collects finished pieces to reduce labor intensity.
6.Three nesting‑cutting modes: Mode‑1 regular neat‑array; Mode‑2 dislocation with reduced‑knife‑count; Mode‑3 dislocation with equal‑knife‑count for better material utilization.
7.Special die‑setting mechanism, calibrate die‑height assisted by 4 mm EVA sheet. Built‑in production counter and I/O signal monitoring for fast fault diagnosis.
Extension: Optimized for mass‑production with infrequent die‑change. Single die dimension limited by moving‑head 350×350 mm. Stable 0.6 MPa air‑supply is mandatory, otherwise material‑clamping unit fails.
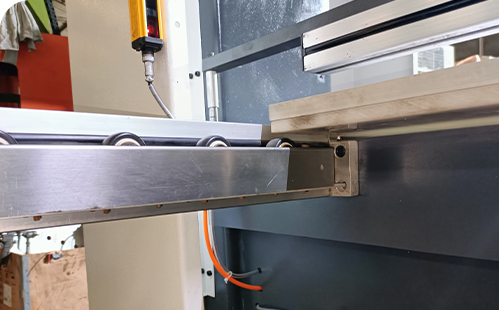
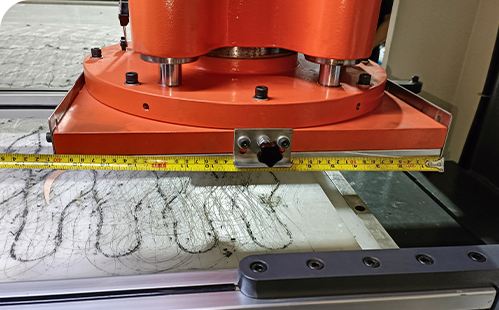
II. Anwendbare Branchen und Werkstoffe
Q4:What products and materials can SY‑830B Automatic Gantry Cutting Machine process?
A4:Process leather, plastic, canvas, nylon, vacuum‑formed material, composite material, sandpaper, medical consumables, shoe sole / upper raw‑material for single‑layer or multi‑layer blanking. Typical products: facial masks, powder‑puffs and other beauty consumables. Extension: For flexible / semi‑flexible materials only. Single die shall not exceed moving‑head size 350×350 mm. Not for metal or rigid hard‑plastic. Optimized for regular‑shape blanks. Not suitable for small‑batch multi‑variant orders with frequent die‑change.
Q5: What production scenarios is SY‑830B Automatic Gantry Cutting Machine mainly used for?
A5:Applied in beauty‑consumable factories, medical‑consumable factories, shoe factories and composite‑material processors for automatic blanking of large‑volume regular‑shape parts with infrequent die‑swap. Up‑stream connects skiving, laminating and rewinding machines. Cut‑parts go to inspection and sewing.
Extension: Focus on low‑labor‑cost automatic‑production. Not recommended for small‑batch frequent die‑change; choose four‑column / flat‑bed cutter for such case.
三. Utility, Installation & Commissioning
Q6: What utility conditions are required for SY‑830B Automatic Gantry Cutting Machine?
A6:Power supply: 3‑phase 220V /50 Hz, reliable protective earthing mandatory. External compressed‑air supply required, stable pressure 0.6 MPa. Floor load‑bearing ≥3400 kg. Check doorway & aisle dimension before delivery due to long machine body. Keep workshop ventilated; keep hydraulic oil away from open fire. Reserve ample space for head cross‑travel, platform movement, die disassembly‑assembly and maintenance. Extension: Machine overall length exceeds 5 m, verify factory passage in advance. Hydraulic oil is flammable; basic fire‑fighting equipment shall be equipped.
Q7:What are requirements for installation & placement of SY‑830B Automatic Gantry Cutting Machine?
A7:Place machine on flat hard load‑bearing floor and level whole unit. Do not stack materials on both sides of gantry‑head travel path to avoid mechanical interference. No obstacles above worktable. Keep away from high‑temperature heat‑source and open fire. Reserve clearance for electric, hydraulic and servo‑guide‑rail maintenance.
Extension: Do not install tight against wall. Keep safety clearance on both sides for traveling‑head stroke.
Q8:What is complete test‑running operating procedure for SY‑830B Automatic Gantry Cutting Machine?
A8:
1.Confirm reliable power earthing. Connect compressed‑air source and confirm stable 0.6 MPa pressure. Fill 80 kg hydraulic oil; verify oil‑pump rotation direction; level whole machine.
2.Switch to 【Manual Mode】, mount die. Use black hand‑wheel plus setting‑switch with 4 mm EVA sheet for die‑height calibration. Extension: Never place hands under cutting‑head during die‑setting.
3.Perform trial cut under manual mode. Increase cutting‑depth parameter by 5 ms per step, do not make large‑step adjustment in one time. Confirm full penetration of trial sample.
4.Move head & feeding‑platform manually, finish 【initial cutting‑position calibration】. Set knives‑per‑row, moving distance, feed‑length, dwell‑hold‑time on touch‑screen; select nesting mode Mode1/2/3; save as recipe.
5.Switch to 【Auto Mode】, home‑reset machine, load raw‑material and start automatic production. Machine stops immediately once safety light‑curtain is blocked.
⚠️Important: Do NOT modify recipe parameters while machine runs automatically. After X/Y‑offset modification: trigger emergency‑stop to clear system memory and re‑home origin point. 6.After production: execute full‑machine home‑reset, stop oil‑pump motor and cut‑off main power. 7.Maintenance procedure: power‑off; wait hydraulic‑system full cooling; place solid support block between cutting‑head and platform before repair work.
Q9: What precautions for recipe‑management & nesting‑mode selection?
A9:Mode1: regular neat‑array for standard nesting. Mode2: dislocation with reduced knives on alternate rows. Mode3: dislocation with equal knives per row. Always save recipe after parameter modification for later recall. Old‑recipe parameters cannot be reused directly after die‑change or material‑thickness change; re‑trial‑cut and re‑calibration is mandatory.
Extension: Die dimension shall not exceed moving‑head dimension 350×350 mm, otherwise mechanical collision will occur.
IV. Maschinenaufbau und Komponenten
Q10:What are the 5 core assemblies of SY‑830B Automatic Gantry Cutting Machine?
A10:5 modular core assemblies:
1.Steel‑gantry frame & feeding‑platform assembly; 2.Servo‑traveling‑head hydraulic cutting unit; 3.Hydraulic pump & oil‑circuit assembly; 4.Pneumatic material‑clamping assembly; 5.PLC‑servo touch‑screen electric‑control system.
‑Steel‑gantry frame & feeding‑platform assembly: steel gantry frame, forward‑backward movable feeding‑platform.
‑Servo‑traveling‑head hydraulic cutting unit: servo cross‑travel mechanism, hydraulic cutting cylinder, die‑clamping mechanism, die‑setting hand‑wheel.
‑Hydraulic pump & oil‑circuit assembly: oil‑pump motor, oil‑tank, solenoid‑valve group, pressure‑regulating valve, oil‑seal sealing‑parts.
‑Pneumatic material‑clamping assembly: material‑pressing bar, air cylinder, pressure regulator (0.6 MPa air source).
‑PLC‑servo touch‑screen electric‑control system: servo driver, touch‑screen HMI, safety light‑curtain, operation buttons, I/O monitoring module.
Extension: Wearing‑parts list: cylinder oil‑seal & O‑ring, high‑pressure oil‑pipe, solenoid‑valve coil, light‑curtain lens, cylinder sealing‑ring. Spare‑part stock recommended to reduce downtime.
Q11: What are respective functions of cutting nesting‑modes Mode1 / Mode2 / Mode3?
A11:Mode‑1: regular neat‑array with aligned die‑positions for general‑purpose production. Mode‑2: dislocation nesting with reduced knife‑count on next row for specific material‑saving layout. Mode‑3: dislocation nesting while keeping equal knife‑count for every row.
Q12: What is function of safety light‑curtain?
A12:Safety protection sensor. Once human limb or foreign‑object intrudes hazardous zone between cutting‑head and platform, machine stops all motion immediately to prevent crush injury.
五.Safety, Maintenance & Troubleshooting
Q13: What safety notes for SY‑830B Automatic Gantry Cutting Machine?
A13:
1.Machine must be reliably earthed for 3‑phase power supply against electric‑shock hazard.
2.Cutting‑head & feeding‑platform run automatically. Never let human‑body enter head‑travel path or hazardous gap between head‑platform. Do not cover, short‑circuit or remove safety light‑curtain.
3.For die‑change & maintenance: cut‑off main‑power; wait hydraulic‑cylinder full cooling; place solid support block under cutting‑head.
4.Do not open protective‑covers under auto‑mode. Do not modify recipe‑parameters during automatic‑running.
5.Inspect pneumatic‑pipe periodically; replace damaged air‑hose timely. Stop machine for troubleshooting when hydraulic‑oil leakage occurs; do not run machine with fault. Extension: Operators shall avoid loose‑sleeves. Do not reach‑in for material during auto‑cycle; pick finished‑goods only after machine stops.
Q14: What is maintenance schedule for SY‑830B Automatic Gantry Cutting Machine?
A14:Per‑shift: Clear debris on platform; keep light‑curtain lens clean; verify 0.6 MPa air‑pressure; inspect hydraulic & pneumatic leakage; test emergency‑stop and light‑curtain safety‑function.
Weekly: Clean and apply grease for servo cross‑travel guide‑rails; inspect cylinder oil‑seal & air‑pipe joints; check tightness of die‑clamping fixture.
Every half‑year: Fasten all electrical terminals; inspect servo‑driver, solenoid‑valve and relay status; check hydraulic‑system condition.
Yearly: Replace hydraulic‑oil and clean oil‑tank & filter; complete‑machine overhaul. Evaluate wear of oil‑cylinder, oil‑pump, servo‑guide‑rail and sealing‑parts; replace aged spare‑parts.
Extension: For long‑term shutdown, lower cutting‑head to low‑position, release residual air‑pressure and apply dust‑proof protection.
Q15: Common faults and troubleshooting guidelines?
A15:
- Uneven cutting‑depth: Re‑perform die‑height setting; verify recipe cutting‑depth & dwell‑hold‑time; check servo home‑origin signal.
- Position offset of servo cross‑travel / feeding‑platform: Clean debris on servo guide‑rail; inspect home‑limit sensor; check signal via touch‑screen I/O‑monitor page.
- Frequent false‑stop triggered by light‑curtain: Lens dust; optical‑path blocked by debris; clean light‑curtain.
- Insufficient cutting‑pressure & incomplete penetration: Low oil‑level; clogged oil‑filter; deteriorated hydraulic‑oil; cutting‑depth parameter set too small.
- Lost recipe‑parameters: 【Recipe‑save】operation not executed after modification. Extension‑added frequent site faults:
- Material‑pressing‑bar no‑action: Confirm air‑pressure reaches 0.6 MPa; check air‑cylinder and solenoid‑valve.
- Cutting‑head no punching‑action: Confirm correct operation‑mode; emergency‑stop reset; check punching‑output‑signal via I/O‑monitor.
- Chaotic motion after parameter‑modified under auto‑mode: Offset‑parameter changed without emergency‑stop to clear memory. Trigger emergency‑stop, home‑reset origin and recall saved recipe.
六.Model Selection
Q16: Which customers are suitable for SY‑830B Automatic Gantry Cutting Machine?
A16:Recommended for beauty‑consumable, medical‑consumable, shoe‑making and composite‑material factories. 30‑ton automatic servo gantry cutter for large‑volume regular‑shape blanks with infrequent die‑change. Up‑stream matches skiving, laminating and rewinding machines. Cut‑parts go to inspection & sewing.
Extension:
✅ Suitable scenarios: Pursue automation & labor‑saving; large‑volume orders; regular‑shape blanks; available 0.6 MPa compressed‑air source; sufficient factory installation‑space.
❌ Unsuitable scenarios: Small‑batch multi‑variant production with frequent die‑swap; die size exceeds moving‑head 350×350 mm; limited workshop‑space and no compressed‑air supply.
Alternative suggestion:
1.Choose AFC‑622 swing‑arm cutter for small‑part sampling.
2.Choose AFC‑525A for medium‑small‑batch manual die‑placement.
3.Choose AFC‑740(40T) / AFC‑780(80T) four‑column cutter for thick‑material heavy‑load cutting.