ASFROM Shoe Delasting Machine FAQ
ASFROM Shoe Delasting Machine FAQ
Shoe Delasting Machine Base Q&A
一.Product Application FAQs
Q1: What production‑process is the AS‑702 double‑station automatic up‑last machine used for?
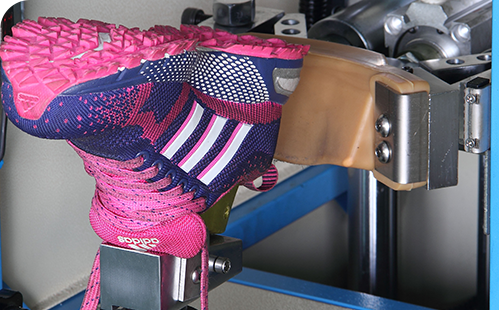
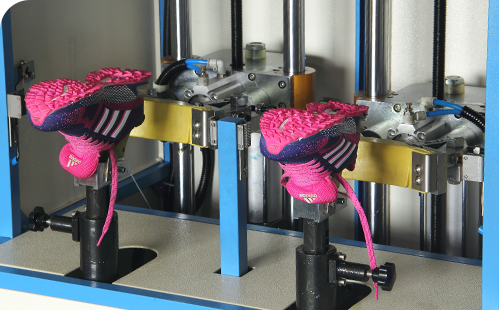
A1: AS‑702 is a dual‑station pneumatic automatic de‑last machine for shoe‑making workshops. It automatically separates finished shoes from shoe lasts. It is applicable to men’s and women’s sports shoes, casual shoes, vulcanized shoes, children’s shoes and other footwear types. It fits mass‑production post‑freezing de‑last working stations.
二. Core Features & Advantages FAQs
Q2: What are the main technical highlights of this double‑station de‑last machine?
A2:
- User‑friendly operation with imported electrical components: Operators only need to place finished shoes onto the last‑setting assembly. The gap between last‑seat assembly and push‑up assembly is adjustable to adapt to different shoe sizes.
- Dual‑head double‑station design: Two independent de‑last modules can work simultaneously or separately. Compared with traditional single‑station hydraulic de‑last equipment, production capacity increases by 3 times and one‑labour cost can be saved.
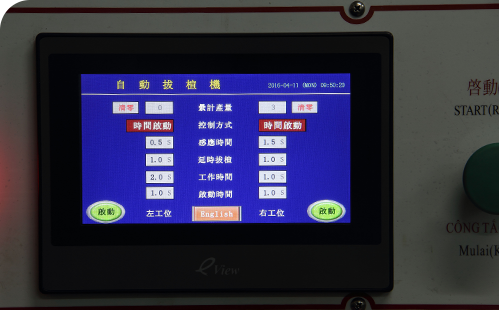
- Photoelectric induction & PLC automatic control: No manual button or foot‑pedal trigger is needed. The machine starts de‑last cycle automatically once shoes are detected. Photoelectric delay time is configurable to match different production speeds.
- Full‑cylinder pneumatic drive: It cancels hydraulic‑oil system. No driving motor is required for executing movement, saving power consumption and eliminating expenses for hydraulic‑oil purchasing and replacement.
- Protective rubber mold: Push‑up de‑last units adopt durable rubber molds. Powerful vertical movement prevents scratches and damages on shoe uppers and guarantees finished‑shoe quality.
三. Complete Technical Parameters FAQs
Q3: What are the complete official specifications of AS‑702?
A3:
| Item | Specification |
|---|---|
| Model | AS‑702 Double Stations Automatic Up Last Machine |
| Working air pressure | 4‑6 KGS |
| Power supply | 220V / 50Hz / 1‑Phase |
| Overall dimensions (L×W×H) | 660 × 820 × 1320 mm |
| Net Weight | 200 KG |
四.On‑Site Installation & Environment Matching FAQs
Q4: What pre‑conditions are required before installation?
A4:‑ Power supply: Stable single‑phase 220V power supply; reliable protective earthing must be completed.
‑ Air supply: Provide clean dry compressed‑air source, maintain working pressure within 4‑6 KGS. Install filter‑regulator unit on air pipelines.
‑ Space allocation: Place on flat solid concrete floor. Reserve enough front operating space for shoe loading‑unloading; keep side clearance for maintenance and adjustment.
‑ Environment: Standard shoe‑factory workshop environment. Avoid heavy‑dust surroundings to protect photoelectric sensors, pneumatic cylinders and electrical parts.
五.Standard Startup & Production Operation SOP FAQs
Q5:What is complete standardized operating procedure from power‑on to mass‑production?
A5:
- Pre‑start‑up inspection: Check power‑supply and earthing status; connect compressed‑air pipeline and inspect pipe joints for air leakage; clean dust on photoelectric sensors; check rubber molds for cracks; confirm all moving assemblies run smoothly.
- Power‑on & parameter setup: Switch on 220V main power and open air‑supply valve. Adjust air pressure to 4‑6 KGS. Set photoelectric induction delay time according to production rhythm. Tune the distance between last‑setting assembly and push‑up assembly for current shoe size. Two stations can be set to work synchronously or independently.
- Idle test‑run: Execute multiple empty cycles. Verify cylinder movement, photoelectric triggering and reset actions for both stations; observe for abnormal noise.
- Sample debugging: Place lasted finished shoes on each station. Observe automatic de‑last performance. Inspect uppers for scratch damage. Fine‑tune gap and delay parameters until de‑last quality meets factory‑internal standards.
- Formal mass‑production: Continuously place shoes on stations, machine will start cycles by sensor trigger. Take out de‑lasted shoes after each action. Perform random sampling inspection regularly.
- Shift‑end shutdown: Stop feeding workpieces. Cut off compressed‑air supply and exhaust residual air. Turn off main power. Clean rubber molds and station surface from shoe scraps and dust.
⚠️ Safety warning: Never put hands into the moving working range during automatic operation to avoid pinching injury. Do not exceed maximum working air pressure of 6 KGS.
六.Common Abnormality & Trouble‑Shooting Tips FAQs
Q6: What frequent‑seen faults may happen in daily workshop, and quick check points for operators?
A6:
• Phenomenon 1: One or both stations do not respond after shoe placement Check points: Check photoelectric sensors for dust or debris covering; confirm air‑pressure stays within 4‑6 KGS; inspect sensor wiring and PLC signal output.
• Phenomenon 2: Insufficient de‑last force, shoe cannot separate smoothly from the last Check points: Appropriately raise working air pressure; inspect rubber molds for heavy wear; re‑adjust positioning assembly spacing; check cylinders for internal air‑leakage.
• Phenomenon 3: Shoe upper gets scratched or torn in de‑last process Check points: Inspect rubber mold surface for burrs and hard foreign objects; correct offset shoe placement; readjust assembly gap.
• Phenomenon 4: Cylinder moves slowly or gets stuck Check points: Check stable air‑supply; inspect pipeline blockage; check aging of cylinder sealing elements.
⚠️ Warning: Operators shall NOT disassemble PLC, pneumatic cylinders and internal electrical assemblies without professional‑technical guidance. Contact supplier‑technical‑support for complex faults.
七.Tiered Complete Routine Maintenance FAQs
Q7: What maintenance items need to be done daily / weekly / monthly?
A7:
✅Daily (before and after each production shift) Wipe photoelectric sensor lenses and rubber mold surfaces; check air‑pipe joints for leakage; test automatic triggering and full‑cycle movement for both stations; clear shoe scraps from positioning assemblies.
✅Weekly Tighten loose mechanical screws; add lubricant for cylinder guide moving parts; inspect rubber molds for tearing and wear; check tightness of electrical terminals.
✅Monthly Re‑calibrate photoelectric delay parameters; comprehensive inspection for pneumatic components and electric‑control system; replace heavily worn rubber mold consumables.
八. Delivered Accessories & Technical Documents FAQs
Q8: What items will be delivered together with the machine?
A8:
- Technical documents (paper hard‑copy + PDF electronic version): Complete English‑language operation manual, electrical schematic diagram, pneumatic circuit schematic diagram, spare‑parts list and common‑fault‑troubleshooting manual.
- Standard delivered accessories: A full set of standard‑tool kit for daily‑machine adjustment and maintenance work; quick‑connect air‑pipe fittings.
九. Warranty Scope & After‑Sales Technical Support FAQs
Q9: What is the exact warranty scope, and which parts are excluded?
A9: 12‑month full‑machine warranty for non‑consumable parts, calculated from goods arrival at buyer’s premises.
Consumable‑wearing parts excluded from warranty: rubber de‑last molds, pneumatic seals, O‑rings, photoelectric sensors. Damage caused by over‑pressure operation, foreign‑object impact and unauthorized disassembly is not covered under warranty.
Q10: What after‑sales technical services are provided?
A10:
- Remote‑video debugging and remote‑fault‑diagnosis service.
- Online‑operator‑operation‑skill‑training guidance; door‑to‑door on‑site service can be arranged as required.
- Lifelong spare‑parts supply at factory‑cost price for customer follow‑up replacement.
- Process‑technical support: assist customers to adjust assembly spacing and induction‑delay parameters for different shoe sizes and shoe‑material constructions.
Supplementary note: Control circuit uses 220V single‑phase power; actuators are fully pneumatic. Working air pressure must be kept between 4‑6 KGS. Two stations support synchronous or independent operation modes.